Sterile medications require an exceptionally controlled manufacturing process because contamination, dosing inconsistencies, or packaging failures can directly affect product quality and patient safety. For pharmaceutical companies developing respiratory, ophthalmic, otic, oral liquid, or other sterile products, choosing an experienced sterile unit dose pharmaceutical manufacturing partner can provide the infrastructure, automation, quality systems, and production scale needed to move a therapy from development into commercial supply.
Unit-dose pharmaceutical manufacturing is built around preparing a precise amount of medication in an individual container intended for a single administration. This format can offer advantages in convenience, dosing accuracy, handling, and contamination control compared with larger multi-dose containers.
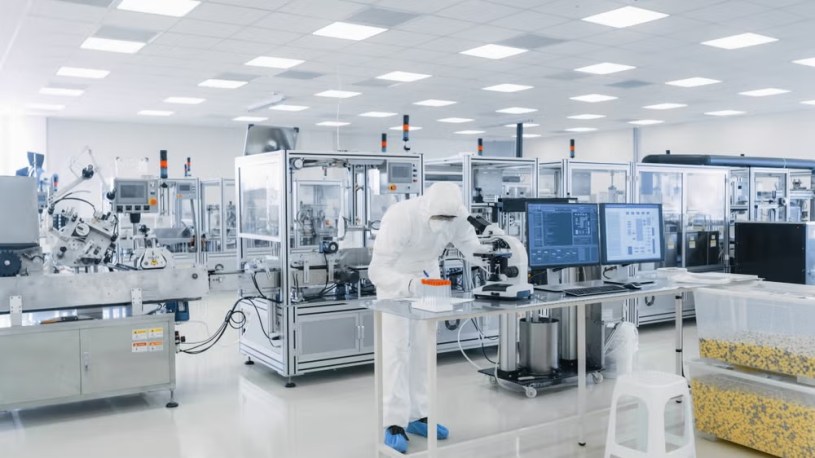
For sterile products, the manufacturing environment becomes particularly important. The product must remain protected from microorganisms and other contaminants throughout filling, sealing, inspection, and packaging. Highly automated systems can reduce unnecessary human interaction during these critical stages.
Blow-Fill-Seal technology is one method used to manufacture sterile unit-dose liquids. In this process, pharmaceutical-grade polymer is formed into a container, filled with the drug product, and sealed within one continuous automated sequence. RiteDose identifies BFS as its core manufacturing platform and describes it as a leading approach for sterile unit-dose delivery.
The process begins with low-density polyethylene polymer, or LDPE, which is formed into the desired container shape. The pharmaceutical formulation is then filled into the newly created container and immediately sealed. Completing these steps within an enclosed manufacturing process can reduce the number of separate handling stages normally required during traditional filling operations.
Automation provides another important advantage. Pharmaceutical filling equipment can operate at high speeds while maintaining repeatable process parameters. For products requiring millions of individual doses, this consistency is essential.
RiteDose currently supports sterile liquid containers with fill volumes ranging from approximately 0.2 mL to 15 mL. Its platform can accommodate applications including inhalation products, eye drops, otic medications, and oral liquids. The company also notes that container molds can be customized according to individual product requirements.
Manufacturing capacity is particularly important as a pharmaceutical program progresses toward commercialization. A therapy that begins with relatively small development batches may eventually require hundreds of millions of individual doses.
A manufacturing partner therefore needs equipment, personnel, quality systems, and facility capacity that can scale alongside demand. RiteDose states that its U.S. facility can produce more than 2.6 billion units annually and includes multiple filling suites, formulation capabilities, and high-speed packaging systems.
Quality control must remain consistent throughout this growth. Pharmaceutical manufacturers need systems for chemistry testing, microbiology, validation, regulatory oversight, and quality assurance. These functions help ensure that every stage of production operates according to established requirements.
Sterility assurance is only one part of product quality. The medication must also be formulated correctly, filled at the appropriate volume, sealed properly, inspected, packaged, and released according to validated specifications.
The package itself also plays an important role. Unit-dose containers must protect the formulation while allowing patients or healthcare providers to administer the medication conveniently. Container geometry, material compatibility, fill volume, and closure integrity all need to be considered during product development.
Blow-Fill-Seal can integrate these packaging requirements directly into the manufacturing process because the container is created at the same time the medication is filled. This differs from processes where pre-manufactured containers must be sterilized, transported, and introduced separately.
Another important consideration is lifecycle support. Pharmaceutical products often require changes or additional manufacturing work after initial commercialization. Demand may increase, new packaging configurations may be introduced, or regulatory updates may require further validation.
A CDMO with development and commercial manufacturing capabilities can help manage these transitions without requiring repeated transfers between different suppliers.
RiteDose positions its CDMO platform as supporting programs from early-stage clinical development through large-scale commercialization, including process validation and lifecycle support. This type of integrated approach can help reduce complexity as a product advances.
Supply reliability also matters because manufacturing disruptions can affect healthcare providers and patients who depend on these medications. High-capacity operations, validated manufacturing processes, quality oversight, equipment maintenance, and experienced personnel all contribute to maintaining a dependable supply chain.
For pharmaceutical companies evaluating sterile unit dose pharmaceutical manufacturing partners, the decision therefore extends beyond filling equipment alone. A capable manufacturer should combine aseptic expertise, scalable production, regulatory support, validation, quality systems, packaging capabilities, and long-term commercial capacity.
Sterile unit-dose manufacturing brings together pharmaceutical science, engineering, automation, and quality control. When supported by Blow-Fill-Seal technology and an experienced CDMO infrastructure, it can provide a practical and scalable way to produce medications that require precise, individually packaged doses.
As demand continues for sterile respiratory, ophthalmic, otic, and other liquid medications, reliable unit-dose manufacturing will remain a critical part of the pharmaceutical supply chain. A manufacturing partner capable of maintaining quality while scaling production can help ensure that approved therapies consistently reach the patients who depend on them.

